Air-to-Air Heat Exchangers & Heat Recovery · Since 2005

Heat Recovery for Lithium Battery Electrode Coating

Energy and solvent in electrode drying

Lithium-ion battery production coats electrode slurry on foil and dries it in long ovens, exhausting hot air carrying the NMP solvent. That exhaust is both an energy stream and part of the solvent-recovery loop, so recovering its heat improves both efficiency and recovery economics.

Suitable exchanger types and how they work

Stainless plate air-to-air exchangers preheat the incoming fresh drying air with the hot exhaust before the stream enters the NMP condensation/recovery stage. A counterflow plate gives the highest preheat temperature. Where oven zones are distant, a run-around coil links them without mixing.

Design considerations for battery lines

The exhaust contains NMP vapor and fine electrode dust. Use stainless, cleanable plates with condensate and solvent drainage, and confirm material compatibility with the recovery process. Keep pressure drop within the oven’s fan budget and design for regular wash-down to avoid dust buildup that would raise energy use.

Boiler Flue Gas Heat Recovery and Plume Abatement

Heat and plume lost up the stack

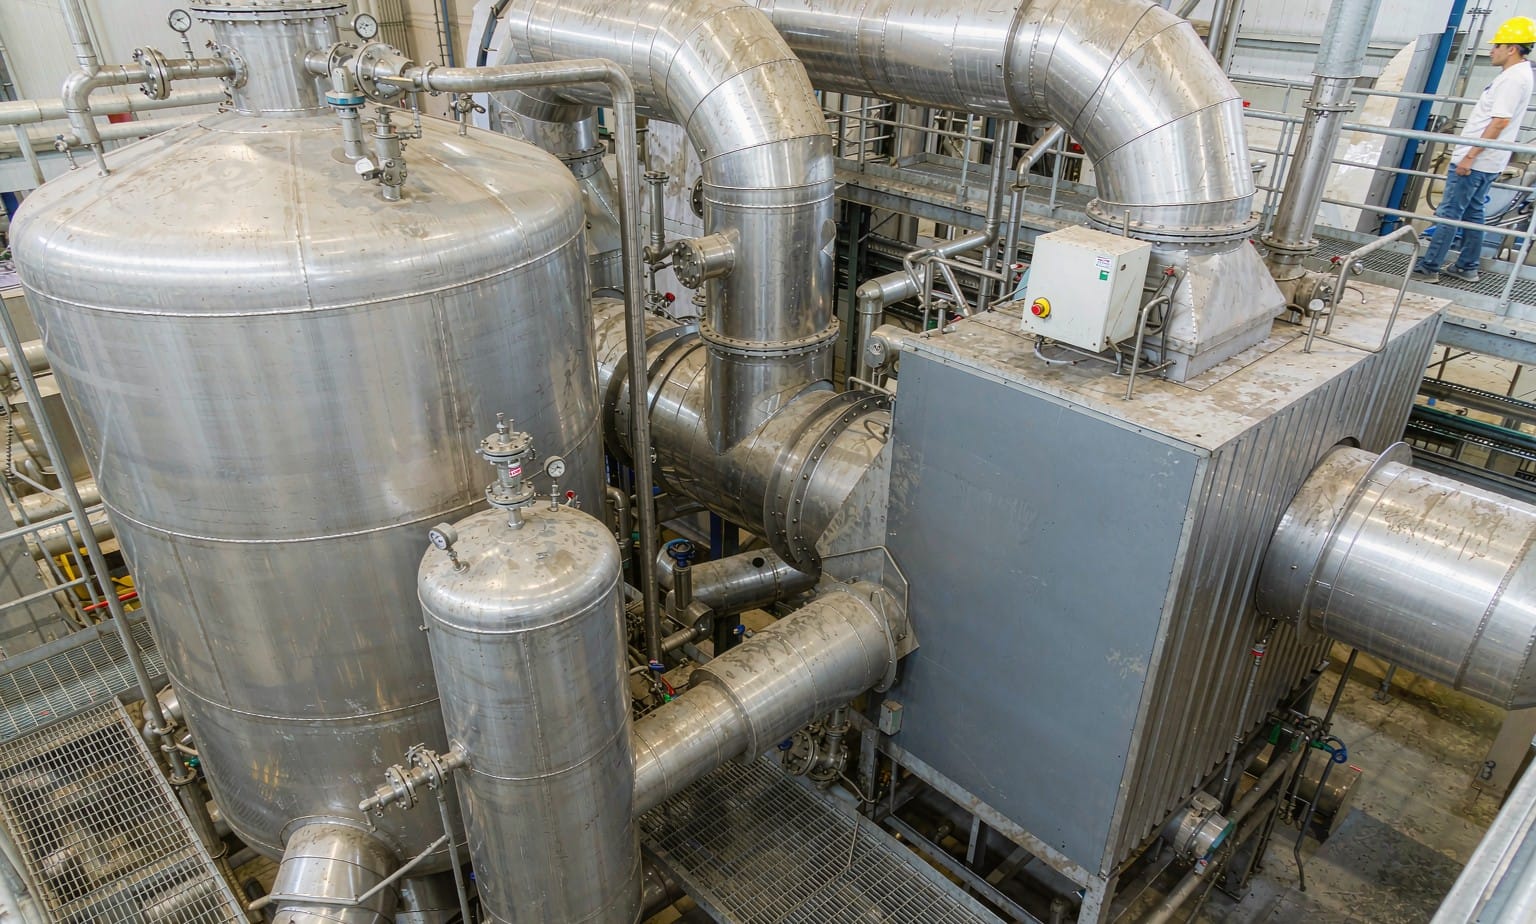
Conventional boilers expel flue gas well above ambient temperature, wasting sensible heat, and the warm, moisture-laden plume can condense into a visible white plume that annoys neighbors. Recovering that heat for incoming combustion air or building heating cuts fuel use and can suppress the plume.

Suitable exchanger types and how they work

A stainless plate air preheater transfers flue-gas heat to the combustion air or a separate heating loop. Running the exhaust below its dew point lets a condensing exchanger also recover latent heat, squeezing more efficiency out of the same fuel. An air-to-water recovery loop is an alternative when water heating is the better sink.

Design considerations for flue gas

Flue gas is corrosive, especially below the acid dew point. Specify stainless or alloy plates, provide condensate collection and neutralization, and protect against low-temperature corrosion. Size for the boiler’s flue volume and pressure drop, and ensure the recovered heat has a real use (preheat, space heating, or process) so the savings are captured.

Heat Exchanger for VOC Abatement Exhaust (RTO/RCO)

Energy demand of thermal oxidizers

RTO (regenerative thermal oxidizer) and RCO (regenerative catalytic oxidizer) units destroy VOC-laden process air at 700-900°C. Reaching that temperature for every cubic meter of incoming air is expensive, so the oxidizer’s own hot exhaust is used to preheat the cold, solvent-laden inlet stream before it enters the burner or catalyst bed.

Suitable exchanger types and how they work

Within an RTO the heat is stored in a ceramic regenerator bed, but the upstream make-up air and the downstream clean-exhaust loops are often linked by a high-temperature air-to-air plate exchanger. This recovers sensible heat from the cleaned exhaust to warm the raw inlet. Our plate core material selection guide helps pick temperature-rated alloys.

Design considerations for oxidizer loops

Temperatures are high and the exhaust can be acidic or contain catalyst fines. Specify stainless or higher-grade alloys rated for the duty, allow for thermal expansion, and design cleaning access for any particulate. Confirm the exchanger’s pressure drop fits the oxidizer’s existing fan and that no cross-leakage contaminates the clean side.

Heat Recovery for Textile, Printing and Coating Dryers

Continuous exhaust from drying lines

Textile stenters, printing presses, and coating/laminating lines run long drying tunnels that exhaust hot air almost continuously. That exhaust carries both sensible and often latent heat, plus solvent or particulate loads. Recovering it preheats combustion or make-up air and can offset the building’s heating demand.

Suitable exchanger types and how they work

High-temperature stainless plate exchangers handle the duty; the exhaust preheats incoming fresh air in a counterflow arrangement for maximum effectiveness. When supply and exhaust paths are remote, a run-around coil moves the energy between them. For lines where humidity control matters, an enthalpy wheel can also recover moisture.

Design considerations for textile and coating

Exhaust may contain fibers, ink solvents, or sizing dust. Use stainless plates with accessible, cleanable surfaces and condensate management, and keep surface temperatures above the solvent dew point where required by safety. Verify pressure drop against the existing exhaust fan, and confirm material compatibility with any solvent vapor present.

Heat Recovery for Sludge Drying

The sludge-drying energy challenge

Reducing the water content of municipal, chemical, and electroplating sludge is energy-intensive, and the exhaust is hot, saturated, and often acidic or salinated. Without recovery, much of the dryer’s heat leaves with the exhaust vapor. An air-to-air exchanger captures that heat to preheat intake air or pre-dry incoming sludge, lowering the load on the primary heater.

Suitable exchanger types and how they work

A closed-loop, sensible plate exchanger is typical: hot humid exhaust preheats the supply air in a separate, clean loop so corrosive condensate never contacts the process air directly. Where the two streams are far apart, a run-around coil links them with a pumped fluid loop and guarantees zero mixing.

Design considerations for sludge duties

Expect condensation loaded with chlorides, sulfates, and organics. Specify stainless steel or epoxy-coated cores, provide condensate neutralization and drainage, and design for frequent cleaning — see our cleaning and maintenance SOP. Corrosion allowance and washable, accessible plates are non-negotiable for a long service life.

Heat Exchanger for Data Center and Telecom Cabinet Cooling

Why data centers need closed-loop recovery

Data centers, telecom base stations, and power-electronics cabinets generate dense heat that must be rejected continuously. Bringing untreated outside air in risks dust, humidity, and corrosion of sensitive electronics. An air-to-air heat exchanger transfers heat from the hot internal loop to a cooler external loop with zero mixing of the two airstreams.

Suitable exchanger types and how they work

Plate air-to-air exchangers and heat-pipe exchangers are both common. Heat pipes need no fans on the device itself and tolerate vertical orientation well, making them popular for cabinet and base-station cooling. Indirect evaporative cooling combines the exchanger with a water-spray side for very low supply temperatures. Our heat-pipe working-fluid selection guide covers the fluid choices.

Design considerations for electronics cooling

Leakage between loops must be near zero, so specify IP-rated, sealed plate cores. Keep internal-loop air clean and dry, watch pressure drop on the fan-powered side, and size for the cabinet’s worst-case heat density. For outdoor cabinets, choose coatings that resist salt fog and temperature cycling.

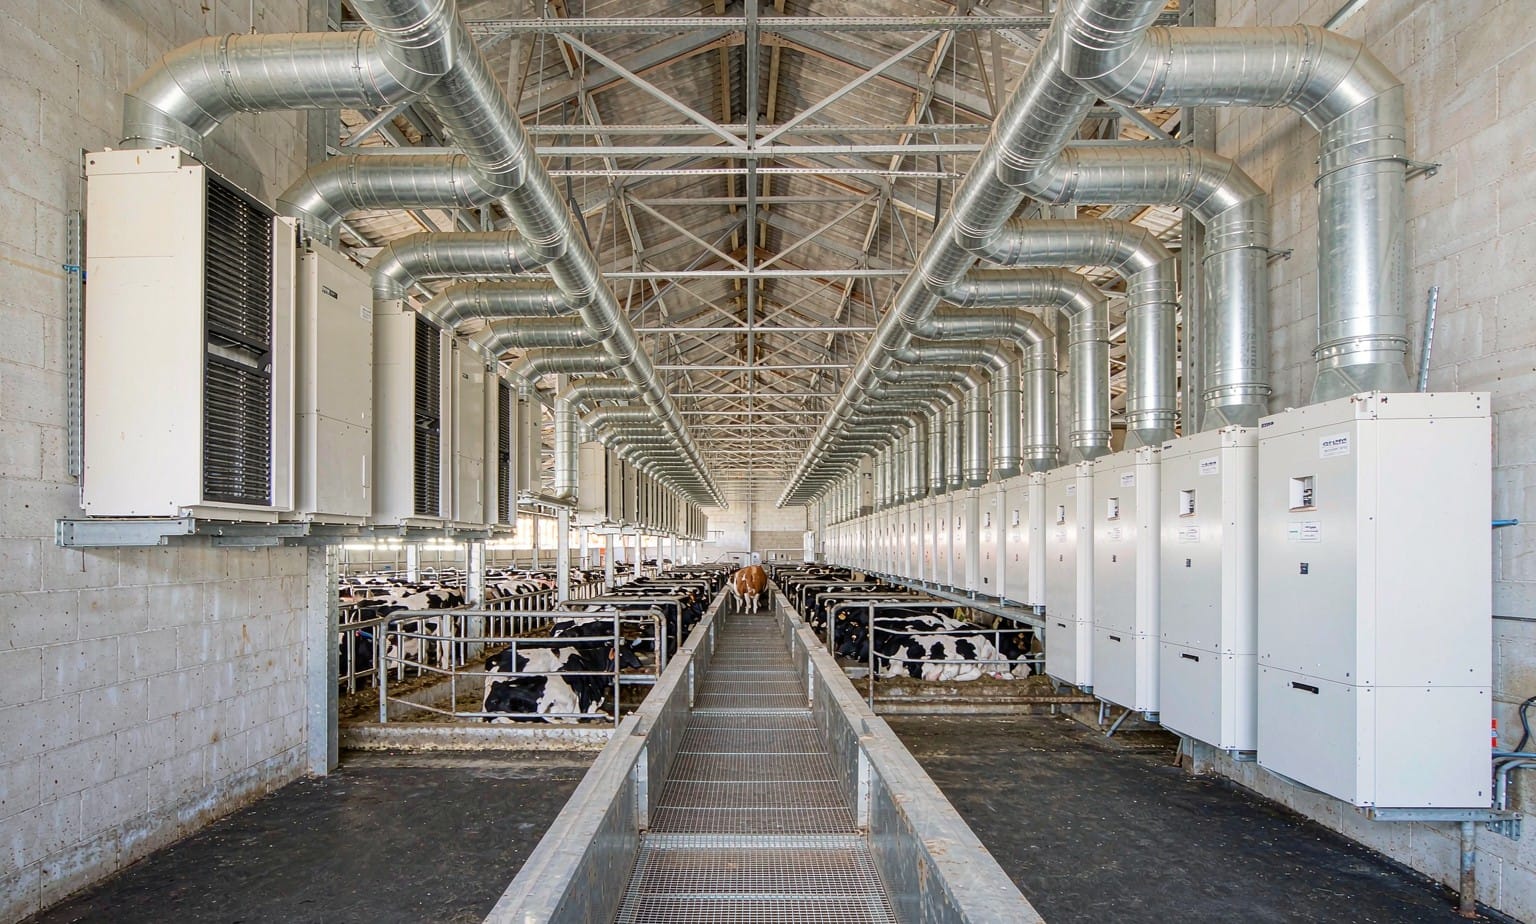
Air-to-Air Heat Recovery for Livestock Barns

The ventilation heat-loss problem

Pig, poultry, and rabbit barns need continuous ventilation to remove ammonia, CO2, moisture, and pathogens — but in winter that ventilation throws away heated indoor air. Cold-climate barns can lose most of their heating energy through the exhaust stream alone. An air-to-air heat-recovery ventilator captures heat from the outgoing barn air and transfers it to the incoming fresh air while keeping the two streams separate.

Suitable exchanger types and how they work

Plate-type heat-recovery ventilators suit most livestock buildings. In cold climates a counterflow plate maximizes recovery and reaches the lowest supply temperature, while a built-in bypass handles summer. Where humidity control matters, an energy-recovery ventilator (ERV) also transfers moisture between streams.

Design considerations for barns

Barn air is corrosive (ammonia) and dusty. Specify epoxy-coated or stainless cores and washable plates, plan condensate management, and add a defrost strategy (bypass or preheat) for freezing nights. Size the unit to the required ventilation rate rather than total airflow, and provide easy access for regular cleaning of the core and drains to keep pressure drop and ammonia exposure under control.

Heat Exchanger for Industrial Drying Ovens

Why drying ovens waste energy

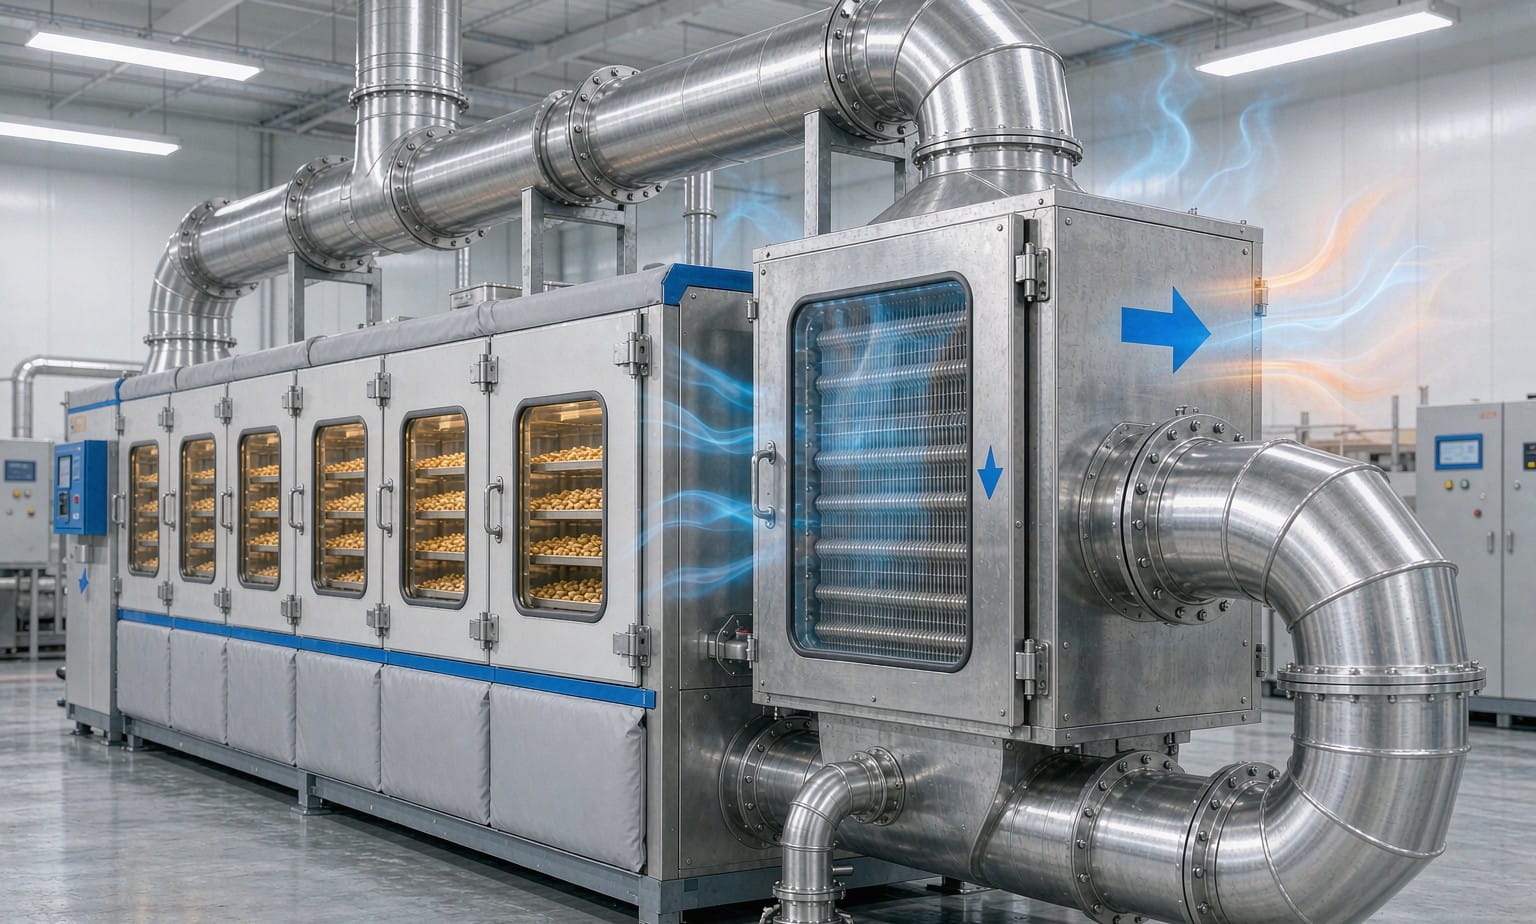
Industrial drying ovens in food, agriculture, and materials processing push large volumes of hot, humid air out as exhaust. That stream can carry 30-60% of the dryer’s thermal input, so every kilogram of water removed also wastes fuel. Fitting an air-to-air heat exchanger lets the outgoing hot, moist air preheat the incoming fresh air before it reaches the oven, directly cutting the burner or electric heater load.

Suitable exchanger types and how they work

Fixed-plate air-to-air exchangers are the usual choice for drying lines because they handle high humidity and keep the two airstreams physically separate — no moisture, odor, or particulate crosses from exhaust to supply. A sensible plate recovers temperature; a membrane or enthalpy plate can also recover latent heat. For very humid duties an enthalpy wheel additionally transfers moisture. Sizing guidance is in our plate heat exchanger selection guide.

Design considerations for drying duties

Drying exhaust is usually loaded with water vapor, dust, oil mist, or fine powder. Choose stainless steel or hydrophilic-aluminum plates that resist corrosion and can be washed, provide condensate drains, and leave service clearance for periodic wash-down. Size face velocity to keep pressure drop acceptable, and consider a summer bypass so the recovered heat does not overheat the process in warm months.

For a practical walkthrough of measuring and verifying savings on a real dryer, see our heat-recovery case-study articles.

EN 13053 - Rating of Air Handling Units (Including Heat Recovery)

EN 13053 specifies requirements for the rating and tolerances of air handling units and their functional sections.

Scope

It addresses components such as filters, coils, fans, and heat-recovery sections, with defined rating methods and permissible tolerances.

The heat-recovery section

The standard treats the recovery section as a rated component, so its effectiveness is subject to the same tolerance discipline as other AHU parts.

Tolerances

Aspect Discipline
Rating method Defined per component
Tolerance Max deviation from rated value
Testing Verification route

Practical use

When procuring an AHU, reference EN 13053 so the recovery section is rated and warranted to a known tolerance, not left as an unverified sub-assembly.

Common pitfall

Specifying recovery effectiveness without an EN 13053 tolerance leaves the supplier free to under-deliver within an undefined band.

ISO 9229 - Thermal Insulation Vocabulary

ISO 9229 defines the vocabulary used in the field of thermal insulation, including terms for heat transfer, materials, and performance.

Why a vocabulary standard

Heat-recovery specs mix terms such as conductivity, resistance, effectiveness, and recuperation. ISO 9229 fixes their meaning so a supplier and buyer mean the same thing.

Useful terms for our field

Term Meaning
Thermal resistance (R) Resistance to heat flow
Thermal transmittance (U) Heat flow per area per temperature diff
Effectiveness Actual / max possible transfer

Effectiveness vs efficiency

In recovery, "effectiveness" is the correct term; "efficiency" is often misused. ISO 9229-aligned wording avoids the ambiguity.

Practical value

Citing standardized terms in your specification reduces disputes over whether a quoted "efficiency" means sensible effectiveness or total effectiveness.

Request a Quote
Need Help?